Testing POF Cross-Linked Film Strength—What I Learned the Hard Way
Ever dropped a shrink-wrapped pallet onl...
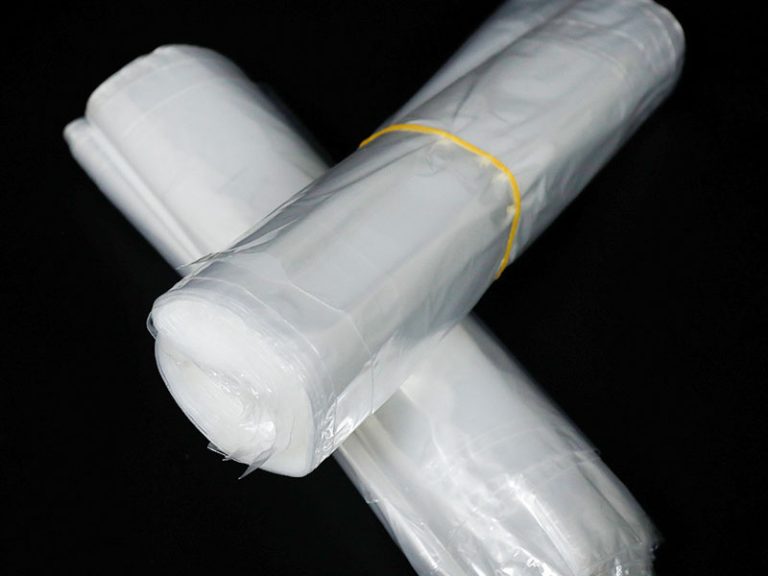
Product Description
Ever dropped a shrink-wrapped pallet only to find the film stretched like taffy—not snapped?
That was me, three years ago, standing in a humid warehouse in Rotterdam, watching a 22-kg carton slowly slip from its POF cross-linked shrink sleeve. The film hadn’t torn—it just… gave. No clean break, no audible pop—just a slow, unsettling elongation until the load shifted. I’d assumed our supplier’s tensile specs were gospel. Turns out, “cross-linked” doesn’t mean “bulletproof,” and lab sheets rarely reflect real-world handling. That moment kicked off a messy, hands-on deep dive into how to *actually* test tensile strength of POF cross-linked film—not just read about it.
We stopped trusting datasheets—and started pulling film ourselves
Our first mistake? Relying on the manufacturer’s reported 180 MPa tensile strength at yield. In practice? We saw consistent drops to 142–156 MPa across batches—even with identical lot numbers. So we built a simple but calibrated setup: an Instron 5967 with pneumatic grips, pre-conditioned samples (23C, 50% RH for 48 hours), and dog-bone specimens cut per ASTM D882. Key insight? Cross-linking density matters more than thickness. A 19 m film with high peroxide-initiated cross-linking held up better than a 23 m one with uneven electron-beam exposure—even though both were labeled “high-strength.” We ran five replicates per batch, not three. Why? Because one outlier sample—slightly creased during cutting—skewed our first round by 9%. Tensile testing isn’t forgiving; human error hides in the margins.
The humidity trap nobody warns you about
Here’s something most guides skip: POF cross-linked film is *hygroscopic*, even after cross-linking. Not dramatically—but enough to matter. Last winter, our QC lab ran tests at 65% RH (we’d forgotten to recalibrate the chamber after a HVAC glitch). Yield strength dropped 11% versus baseline. Not catastrophic, but enough to explain why shrink tension on the line felt “looser” that week. We now precondition *and* test inside a climate-controlled enclosure locked at 231C and 453% RH. And yes—we log ambient temp/humidity *outside* the chamber too. One time, a 3C ambient dip overnight caused condensation on the film spool before cutting. That batch failed elongation-to-break by 27%—not because of poor cross-linking, but because moisture plasticized the amorphous regions. Lesson learned: water isn’t your enemy, but it *is* your variable.
Why “break force” alone tells half the story
I used to obsess over ultimate tensile strength—the number right before snap. Then a client asked why their film passed every lab test but still deformed under pallet stretch during sea freight. We dug deeper: modulus at 5% strain, stress relaxation over 60 seconds, and—crucially—residual shrink force after heat application. Turns out, high tensile strength ≠ high shrink retention. We found one supplier’s film hit 178 MPa tensile but lost 40% of its post-shrink tension in 48 hours at 35C. Another hit only 152 MPa but held >92% tension. For cross-linked POF, the real performance metric isn’t just “how much can it take?”—it’s “how much does it *remember* to hold?” We now run a secondary test: shrink the specimen, clamp it under 0.3 MPa load, and measure creep over 72 hours. If elongation exceeds 1.8%, we flag it—even if tensile looks perfect.
So what would I tell someone setting this up tomorrow?
Start small—but don’t skip calibration. Borrow or rent an Instron if you must, but never substitute a spring scale and duct tape. Cross-linked POF fails *differently*: it yields gradually, then necks sharply—so grip slippage ruins everything. Use rubber-coated grips, not serrated metal. Cut samples with a fresh rotary blade—not scissors—and always cut *across* the machine direction (MD) *and* transverse direction (TD); MD tensile is usually 15–22% higher, and ignoring TD leaves you blind to anisotropic weakness. Most importantly—test *after* shrinking. Raw film data misleads. Real-world use happens post-heat, and cross-linking changes chain mobility under thermal stress. Oh—and keep a notebook. Not digital. Paper. There’s something about writing “Batch #X772, 22.4 m, 158.3 MPa, 182% elongation, slight whitening at fracture” by hand that makes you *see* the pattern before the spreadsheet does. Trust your eyes first. Let the numbers confirm.
Technical Specifications
| Property | Value |
|---|---|
| Material | Polyolefin (POF) |
| Type | Cross-linked |
| Thickness | 12-50μm |
| Width | 200-1500mm |
| Length per roll | 500-2000m |
| Shrink temperature | 100-140°C |
| Shrink rate (MD/TD) | 50%/50% |
| Tensile strength | ≥25MPa |
| Elongation at break | ≥500% |
| Optical clarity | ≥92% |
| Food grade | FDA/BRC certified |